Stick Electrodes
Explore our wide range of stick welding electrodes designed for precision, durability, and versatility across various applications. From carbon steel to specialty alloys, our solutions meet the demands of diverse industries with reliable performance and superior weld quality.
Carbon Steel
Low Alloy
Stainless Steel
Nickel-Copper Alloy
Cast Iron
Inconel
Carbon Steel Electrodes
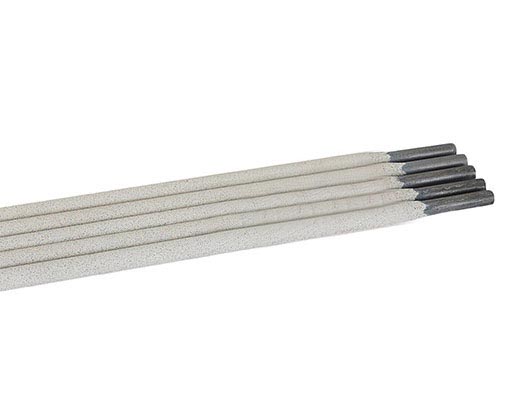
WP Alloys’ carbon steel stick electrodes are designed for general welding applications with a great welding performance. These electrodes are classified as cellulosic electrodes and mild steel electrodes.
Cellulosic electrodes are welding electrodes that are covered in a coating that contains organic materials. The main features of Cellulosic Electrodes are deep penetration and able to weld metal with good mechanical properties.
Mild steel electrodes offer a quiet and stable arc, that offers low penetration which makes them ideal for bridging wide gaps and for working with thin plates. There are, however, various types of mild steel electrodes, each of which has slightly different properties which make them better suited for different applications.
Our carbon steel electrodes are design with the best welding properties to get the best suited for welders.
Below a short sample of the products on this category.
| Product | AWS / ASME | Descripton |
|---|---|---|
| 6010 | A 5.1 E6010 | E6010 has a thick flux coating and fast-freeze slag system designed to withstand contaminated metals and prevent porosity. It offers deep penetration capabilities thanks to its higher current capacity and forceful arc. You can use it for root passes in pipe welding and fabrication. |
| 6011 | A 5.1 E6011 | E6011 is a mild steel, all position electrode designed primarily for use on AC power sources. It produces a strong arc force for deep penetration and a fine spray transfer that enhances operator appeal. Fast freezing or rapid solidification of the metal allows welding in the vertical and overhead position. |
| SUPER RED 6013 | A 5.1 E6013 | E6013 is best used for light to medium penetration on thin or sheet metal pieces. E6013 electrodes are commonly used in manufacturing truck frame bodies, metal furniture, storage tanks, farm implementations, or where aesthetics are critical. |
Please contact us for further information on the above and other products.
Low Alloy Electrodes
Our low alloy steel stick electrodes are engineered for welding high-strength steels and critical structures, providing excellent mechanical properties and crack resistance.
A low hydrogen electrode is essentially a Shielded metal arc welding (SMAW) consumable that contains a moisture content of less than 0.6%, compared to the more traditional 4-6% moisture content found in cellulosic electrodes. These electrodes produce smooth, finely rippled weld beads with low hydrogen content, enhancing the quality and durability of the welds.
Our low alloy electrodes as E7018 offer the user low spatter levels combined with a smooth, stable and quiet arc. These features make our electrodes a great choice for welders.
Below a short sample of the products on this category.
| Product | AWS / ASME | Descripton |
|---|---|---|
| 7018 | A 5.1 E7018 | E7018 is the most efficient general purpose, iron powder-low hydrogen electrode used for welding carbon steels, free-machining steels and low alloy steels with a minimum yield strength of 50,000 psi. The H4 means that the hydrogen level in the all weld metals is below 4 ml per 100 g weld metal. This hydrogen level will avoid hydrogen induced cracks. The “R” indicates that the product has undergone specific testing and the filler metal manufacturer has deemed it to be moisture-resistant. The addition of a “-1” means that the product offers additional impact values to resist cracking at lower temperatures. The addition of a A1 means a low hydrogen iron powder type electrode yielding a weld deposit containing 0.5%Mo. Ideal for welding creep resistant C-Mo steels for service temperatures up to 525°C |
| 7018H4 | A 5.1 E7018 H4 | |
| 7018H4R | A 5.1 E7018 H4R | |
| 7018-1H4R | A 5.1 E7018 -1 H4R | |
| 7018-A1 H4R | A 5.1 E7018 –A1 H4R | |
| 7024 | A 5.1 E7024 | E7024 is a high speed, iron powder, heavy coated electrode for high deposition rates on horizontal and down hand welding. |
| 8018 B2 | A 5.5 8018-B2 | E8018 B2 is an iron powder, low hydrogen type electrode. Its coating contains much iron powder, increasing working efficiency. Owing to this high working efficiency, it is most suitable for welding thick steam pipes and repair welding of cast steel. |
| 8018 C3 | A 5.5 E 8018-C3 | E8018-C3 is an outstanding all position low hydrogen electrode designed for welding high strength steels and applications needing 1% nickel. |
| 9018 B3 H4R | A5.5, E9018-B3 H4R | E9018 B3 basic coated low hydrogen welding electrode for welding of 2.25% Chromium and 1% Molybdenum alloyed steels subjected to elevated temperatures, such as those found in power piping and boilder industries |
| 11018 | A5.5, E11018- H4R | E11018 is an outstanding electrode designed for use in Military applications which require weld joints with 116 ksi minimum tensile strength. |
| 12018 | A5.5, E12018- H4R | E12018 is recommended for use in fabrication of low-alloy, high tensile steels where welds of 120 ksi (830 MPa) minimum tensile strength are required. |
Please contact us for further information on the above and other products.
Stainless Steel Electrodes

WP Alloys’ stainless steel electrodes are engineered for diverse welding applications, including joining dissimilar steels, overlaying on manganese steels, and constructing high-temperature and corrosion-resistant structures.
Below a short sample of the products on this category.
| Product | AWS / ASME | Descripton |
|---|---|---|
| 307-16 | A 5.4 E307-16 | E307-16 welding electrode is used for welding ultra-low-carbon stainless steel structures such as 00Cr19Ni9, 0Cr18Ni10Ti etc. with good impact toughness under -196℃ and suitable for welding LNG tanks and pipelines. |
| 308H-16 | A 5.4 E308H-16 | E308H-16 stainless steel welding electrode is an electrode specially designed for producing 19Cr-10Ni weld deposit with carbon 0.04- 0.08%, weld metal is resistant to crack and exhibits excellent mechanical properties at elevated temperature. |
| 308L-16 | A 5.4 E308L-16 | E308L electrode is a mild steel arc welding rod designed to be used with an AC or DC welding current system. It is classified as an austenitic alloy, meaning it contains higher levels of chromium and nickel than other stainless steel alloys.2 |
| 309L-16 | A 5.4 E309L-16 | E309/309L-16 is a stainless steel electrode idea; for joining stainless steels to themselves or to carbon and lo-alloy steels. Carbon content in the weld metal is held to 04% max which gives it increased resistance to intergranular corrosion. |
| 310 | A5.4 E310-16 | E310-16 electrodes were developed for the welding of type 310 stainless steel; weld deposit will exhibit the same chemical analysis and oxidation resistance as the base plate metal. E310-16 is considered a general purpose electrode for welding almost every analysis of carbon and alloy steel. |
| 312 JETBLUE | A 5.4 E312-16 | E312-16 electrodes were originally designed for the welding of high tensile alloys to high temperature heat-resisting alloys on turbo-jet engines. 312 is a good choice for welding carbon steels to stainless, tool steels and other difficult to weld steels. |
| 316L-16 | A 5.4 E 316L-16 | E316/316L-16 is used for welding type 316L or 318 stainless steels. It has a maximum of . 04% carbon content in the weld metal, which reduces the possibility of carbide precipitation and consequent intergranular corrosion. This electrode is widely used in the welding of chemical equipment. |
| 410 | A 5.4 E 410-16 | E410-16 is designed to weld stainless steels of similar chemical composition as well as to overlay carbon steels to impart corrosion, erosion, and abrasion resistance. |
| 410 NiMo | A 5.4 E 410NiMo-16 | E410NiMo-16 is an electrode designed to weld materials of similar chemical composition in cast and wrought forms. 300⁰F preheat and interpass temperatures are recommended when welding with this alloy. Typical Applications: Turbines, valve bodies, high pressure piping, offshore, power generation. |
Please contact us for further information on the above and other products.
Nickel-Copper Alloy Electrode
We offer a variety of nickel electrodes designed for welding pure nickel, providing excellent heat and corrosion resistance. Additionally, our copper electrodes are engineered to resist corrosion, cavitation, erosion, and metal-to-metal wear.
Below a short sample of the products on this category.
| Product | AWS / ASME | Descripton |
|---|---|---|
| NiCu-7 | A 5.11 E NiCu-7 | ENiCu-7 is a flux coated electrode designed for welding of nickel-copper Monel 400 and 404 to themselves and to steel. Perfect for joining many nickel-copper alloys to copper, nickel-copper, carbon steel, and low alloy steel. |
| ECuSn-C | A 5.6 E CuSn - C | ECuSn-C (Phos-Bronze C) welding electrode is excellent for joining copper base alloys not only to themselves but to stainless steel, cast iron, steels. This electrode may be used on AC current and as an electric brazing rod. |
Please contact us for further information on the above and other products.
Cast Iron Electrodes
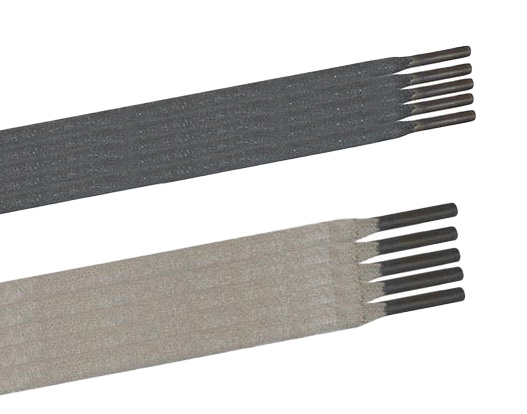
WP Alloys’ cast iron are designed for welding cast iron materials. Suitable to use in repair of machine frames, machine housings, machine parts and bearing blocks. The electrode has a very soft, regular fusion, and a quiet and steady arc. These electrodes are formulated to provide good fusion and reduce the risk of cracking, which is a common challenge when welding cast iron due to its brittle nature.
Below a short sample of the products on this category.
| Product | AWS / ASME | Descripton |
|---|---|---|
| EST | A 5.15 EST | EST is a non-nickel, nonmachinable cast iron electrode. It is the most economical way to go for repairing various kinds of cast iron precincts. |
| ENi55 | A 5.15 E NiFe-CI | ENi55 electrode is designed for welding of cast iron to themselves, as well as joining them to mild steels and repair of castings. |
| ENi99 | A 5.15 E Ni-CI | ENi99 welding electrode is designed for welding gray iron castings to themselves as well as joining them to mild or stainless steels. |
| ENiFe310 | A 5.15 E Ni-CI | ENiFe310 is a Basic-graphite special coated electrode with a bimetallic ferro-nickel core wire which allows very fast fusion on direct current as well as on alternate current without any risk of overheating. Suitable for joining all types of grey cast iron and also for joining cast iron with steel, but especially for nodular cast iron. |
Please contact us for further information on the above and other products.
Inconel Electrodes

WP Alloys’ Inconel electrodes are suitable for chemical processing, marine, aerospace, and other uses. Our products have excellent high-temperature strength and oxidation resistance and can meet stringent radiographic requirements.
Below a short sample of the products on this category.
| Product | AWS / ASME | Descripton |
|---|---|---|
| NiCrFe-2 | A 5.11 E NiCrFe-2 | ENi-CrFe-2 is a nickel-chromium-iron flux coated electrode designed primarily for welding of Incoloy® 800 to itself or to 9% nickel steels. |
| NiCrFe-3 | A 5.11 E NiCrFe-3 | ENiCrFe-3 is a nickel based electrode for welding Inconel 600 and similar Inconel alloys, cryogenic steels, martensitic to austenitic steels, dissimilar steels, heat resisting steel castings of limited weldability |
| NiCrMo-3 | A 5.11 E NiCrMo-3 | ENiCrMo-3 is a nickel-chromium-molybdenum electrode designed for welding of Inconel® 625 or 601, for high strength welds on 9% nickel steels, and for overlaying carbon steel. Used for joining dissimilar combinations of steels or stainless steels to nickel-iron-chromium alloys, such as Incoloy® 800 or 801. |
| NiCrMo-4 | A 5.11 E NiCrMo-4 | ENiCrMo-4 is a low carbon nickel-chrome-molybdenum alloy of type alloy C-276. It is a versatile alloy with excellent wet corrosion resistance in oxidizing and especially in reducing media. |
Please contact us for further information on the above and other products.